Hey everyone, it’s Jake from the component team here, and today I wanna talk about something that comes up every single week from our clients, big and small: 1.20mm pitch components. Like, why do some builds work flawlessly with these, and others end up with weird solder joints, skewed parts, or even full-on failures? Most folks overlook that these tiny buggers have super specific installation needs—nothing crazy, but skip a step, and you’re kicking off headaches you don’t need. Since we’ve been supplying these little guys for years, I’ve seen it all, so let’s break this down real, no-jargon talk. 1.20mm Pitch
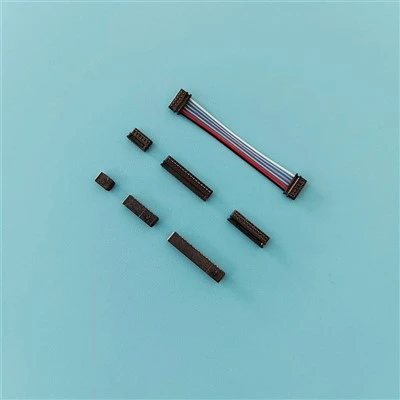
First off, let’s make sure we’re on the same page: 1.20mm pitch just means the distance between the center of two adjacent leads (for through-hole) or pads (for surface mount, which is way more common these days) is 1.20 millimeters. Yeah, that’s tiny—like, smaller than a grain of table salt for the tiny parts, so every measurement matters. The biggest mistake I see install teams make is treating these like they’re 2.54mm pitch (the old-school big ones we all cut our teeth on). Those are forgiving; these are not. So let’s start with the basics that even some seasoned techs sleep on.
First, equipment calibration. This is non-negotiable, full stop. I don’t care if your pick-and-place machine is a $20k industrial rig or your buddy’s fancy hand-soldering setup in his garage—if it’s not calibrated for 1.20mm, you’re wasting time. Let’s do the numbers for pick-and-place first. The nozzle accuracy needs to be within ±0.05mm. Wait, that’s half a tenth of a millimeter—if your machine is off by 0.1mm, you’re already crossing two pads instead of hitting one, or skewing a part so bad it’ll lift when you solder. We get so many returns because a client’s pick-and-place was calibrated for 0.5mm pitch last week, and they just swapped in 1.20mm without tweaking. For hand-builders, if you’re using a vacuum pen, make sure the suction pressure is set right. Too high, and you’ll bend those thin leads on fine-pitch connectors. Too low, and you’ll drop the part mid-placement, which is a disaster when you’re working on a 10,000-unit run. Oh, and for stencils—if you’re using screen printing for solder paste, the stencil thickness is huge. 0.12mm is the sweet spot here. Go thinner, and you’ll have insufficient solder. Go thicker, and you get bridging between leads. We see this all the time: someone uses a 0.15mm stencil because it’s leftover from 0.8mm parts, and suddenly 10% of their boards are shorted.
Next, component handling. These things are delicate, plain and simple. 1.20mm pitch parts have super fine leads and thin plastic bodies, and even static is enough to fry them. Let’s start with ESD protection. Most new techs think ESD is just for semiconductors, but no—these fine-pitch parts can get static-damaged too, even if they look fine. We’ve had a client toss a tray of parts because they forgot the ESD mat, and half were dead on arrival. So: ESD-safe work surfaces, ESD straps for anyone touching the parts, no loose fabric around the workbench, and store them in their original anti-static packaging until the second you’re ready to use them. Don’t pour a whole tray out and let them sit for an hour—pick one at a time, place it, then grab the next. Also, lead bending? Only use the terminals they give you. Some techs try to bend leads to fit their board, but on 1.20mm, that’ll cause micro-cracks in the lead or the plastic housing, which only show up after the product ships. If your board’s footprint is off, fix the footprint—don’t mess with the part. We get way fewer complaints when clients adjust their gerbers than when they bend leads.
Now, solder process. This is where 90% of the mistakes happen. Let’s split this into reflow soldering (the go-to for most surface mount boards) and hand soldering (for prototypes or small runs). Reflow first: the profile is make or break. For 1.20mm pitch parts, you can’t use the same profile as a 2.54mm through-hole part. The preheat phase needs to be slow—ramping at 1-2°C per second, not 5 like you’d do for bigger parts. If you ramp too fast, the flux on the solder paste bubbles, and you get solder balls or bridging. Also, the peak temperature should be 25-30°C above your solder alloy’s melting point (usually lead-free, since that’s standard now—217°C for SnAgCu). Don’t go higher than 260°C, and hold it there for only 10-15 seconds. Longer than that, and the plastic part will warp, or the leads will pull away from the pads. Wait, and solder paste type: use a no-clean, fine-pitch solder paste with a particle size of Type 4 or Type 5. Type 3 is too big, and it won’t flow correctly into those tiny gaps between 1.20mm pads. We always send a quick note with every shipment recommending the right paste, but some clients ignore that and wonder why their joints are crummy.
Hand soldering is even trickier, especially for fine-pitch connectors or resistors. If you’re doing this, don’t use a big iron tip. A 0.3mm conical tip is the max—anything bigger will touch two pads at once, causing a short. Temperature settings: 300-350°C, not higher. Too hot, and you’ll melt the plastic in 2 seconds. Also, use a fine-tip soldering iron, and flux—lots of flux. Rosin-core flux works, but liquid flux is better for fine-pitch because it gets in the tiny spaces between leads. Here’s a pro tip from our lead tech: when soldering, touch the iron to the pad first, not the lead. Let the pad heat up, then add a tiny bit of solder, then bring the lead down. Don’t melt solder on the iron and drag it across the leads— that’s how you get bridging. And for multiple leads, like on a 1.20mm pitch connector, work one lead at a time, or use hot air for the whole thing if you’re comfortable with that. Hot air at 350°C with a fine nozzle, held 5-10mm away, is way faster and more even than hand soldering for parts with 8+ leads.
Board footprint design—wait, a lot of people think this is just a board designer thing, but it’s critical for installation too. The pad size for 1.20mm pitch parts should be around 0.6-0.7mm, right? If pads are too big, bridging is super easy. Too small, and you don’t have enough solder for a strong joint. Also, keep the clearance between adjacent pads at 0.4mm minimum. We’ve seen footprints where the clearance is only 0.2mm because the designer thought it was fine, and when you put solder down, it just bridges automatically. Oh, and make sure the board is flat—no warped PCBs. If your board is warped, the 1.20mm parts won’t sit flush, and you’ll get uneven joints, cold joints, or parts lifting during reflow. We always tell clients to check their PCB flatness before populating, especially for prototype runs where boards might not be milled perfectly.
Wait, what about inspection? You can’t just assemble the board and call it done. For 1.20mm pitch, a visual check with the naked eye only works if you’re a pro. You need a magnifier—10x magnification minimum, or a microscope for high-volume runs. Check for bridging between leads, insufficient solder, skewed parts, and any tiny solder balls. We’ve even had clients miss a tiny bridge on a 1.20mm connector that caused a whole product to fail in the field, so inspection is non-negotiable. For high-volume, automated optical inspection (AOI) is worth the cost. It’s not expensive, and it catches issues you’d miss.
Now, common myths I hear all the time. Myth #1: “1.20mm pitch is the same as 1.25mm pitch.” No, that’s a 0.05mm difference, which is huge. 1.20mm is standard for certain connectors and resistors, 1.25 is for others—mix them up, and the part won’t sit right. Myth #2: “Lead-free solder is fine, no need to adjust.” Lead-free needs higher temps, but as we said, don’t go over 260°C. A lot of techs crank the temp up because lead-free is thicker, and that’s when warping happens. Myth #3: “You can rework 1.20mm pitch parts easily.” Rework is possible, but you need the right tools. A hot air rework station with a fine nozzle, and you have to heat evenly around the part—don’t blast one spot, that’ll melt the plastic. Also, after rework, you have to clean the flux residue, which can be trapped in the small gaps. We recommend practicing rework on scrap boards before doing it on a production run.
Let me wrap this up with a quick recap, because I know that was a lot. Calibrate all your equipment before you start—pick-and-place, stencils, irons. Handle the parts with ESD protection, no bending leads. Use the right reflow profile or hand soldering setup, with fine-pitch solder and the right tip. Design your board with the correct pad sizes and clearances. Inspect every joint properly. That’s it—nothing fancy, just paying attention to the tiny details that make these parts work.

If you’re working with 1.20mm pitch components and running into issues, or you need reliable parts for your next project, don’t overcomplicate it. Reach out to our team—we’ve got years of experience working with install teams to make sure everything goes smooth, from prototype to full production. We can send over a quick installation checklist, answer any questions about your specific part, or work with you to troubleshoot whatever’s slowing you down. No hidden hoops, no confusing scripts—just actual help from people who know these parts inside and out.
0.80mm Pitch References
IPC-A-610, Acceptability of Electronic Assemblies
IPC-J-STD-001, Requirements for Soldered Electrical and Electronic Assemblies
Supplier Technical Notes: 1.20mm Pitch Surface Mount Components, 2023
Dongguan Yinglian Electronics Co., Ltd.
As one of the most professional 1.20mm pitch suppliers in China, we have world-leading production equipment and strong manufacturing capabilities. We warmly welcome you to buy bulk high quality 1.20mm pitch at competitive price from our factory.
Address: No.12, Jidele Road, Juqi, Humen Town, Dongguan City, Guangdong Province, P.R. China
E-mail: James@csg-china.com
WebSite: https://www.csg-conn.com/
